Product Descriptions
Vibrowest Vibrating Screens for Classification - Products and Technical Details
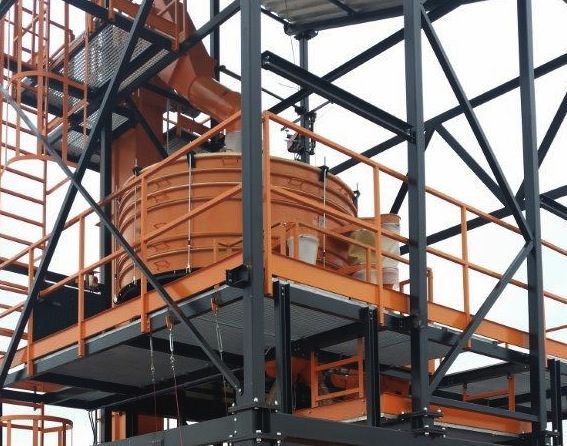
Vibrowest Vibrating Screens for Classification are vibrating separation screens developed for size-based separation, classification, and dust removal in industrial processes. These machines deliver high efficiency and precision in the separation of powders, granules, and dry products with different particle sizes, and they are suitable for use across a wide range of industries.
These classification screens are designed with a customizable structure according to process requirements, and within Vibrowest's extensive product range they include circular, tumbler, and rectangular-type models.
General Technical and Design Features
• Precise Classification: Vibrating screens optimized for particle-size-based separation.
• Advanced Vibration Mechanics: Classification efficiency is increased through different vibration patterns.
• Modular Design: Customization according to process requirements with various model and size options.
• Easy Maintenance and Cleaning: Reduced maintenance time thanks to removable meshes and a stable construction.
• Wide Industry Compatibility: Broad application support for food, pharmaceutical, metal powder, chemical, plastics, agriculture, mining, recycling, and other industries.
Main Models and Technical Features
MR Circular Vibrating Screener
The MR circular vibrating screener is one of the most widely used classification models and effectively separates dry powders and granules.
Technical Features:
• Application: Separation of wet and dry products, control screening, and dust removal.
• Particle Size: Suitable for the separation of fine powders down to 25 microns.
• Operating Principle: Generates both horizontal and vertical vibration components, gently rotating the product across the mesh; vibration is optimized via flywheel balancing weights.
• Capacity: Allows up to five separations within a single machine thanks to its multi-deck capability.
• Construction: Available in AISI 304, 316L, or 316Ti stainless steel; can be integrated with CIP systems and automatic mesh cleaning solutions.
• Model Diameters: Available in various sizes ranging from Ø 400 mm to Ø 2200 mm.
Thanks to its design, this model enables effective separation of both very fine powders and granular products.
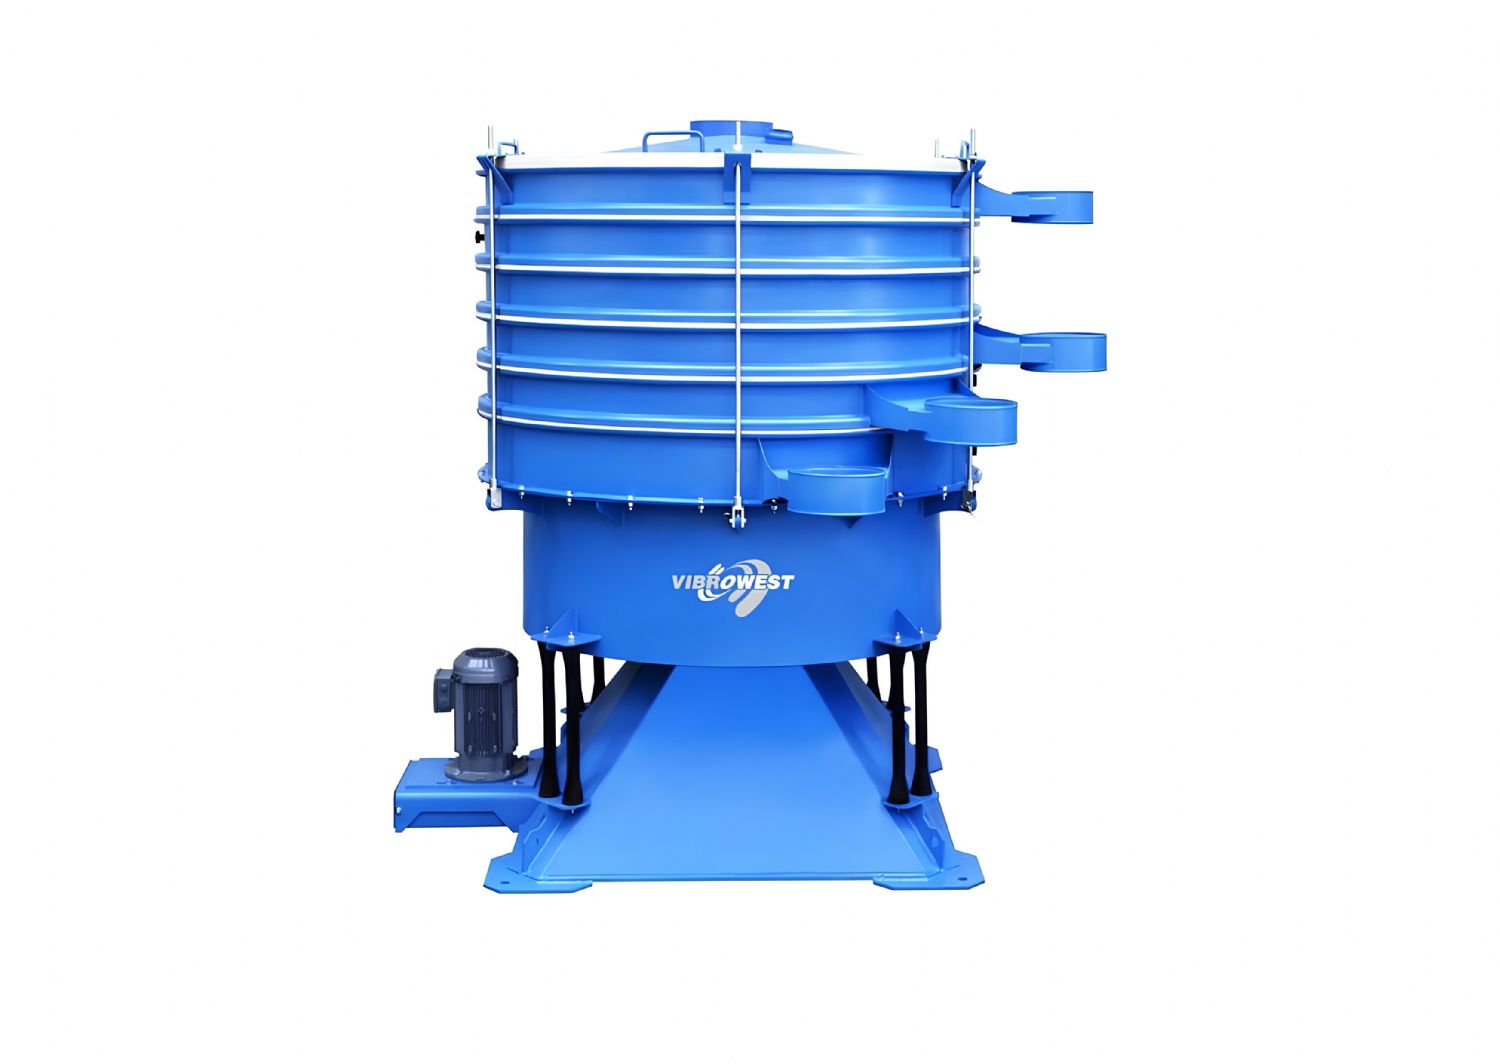
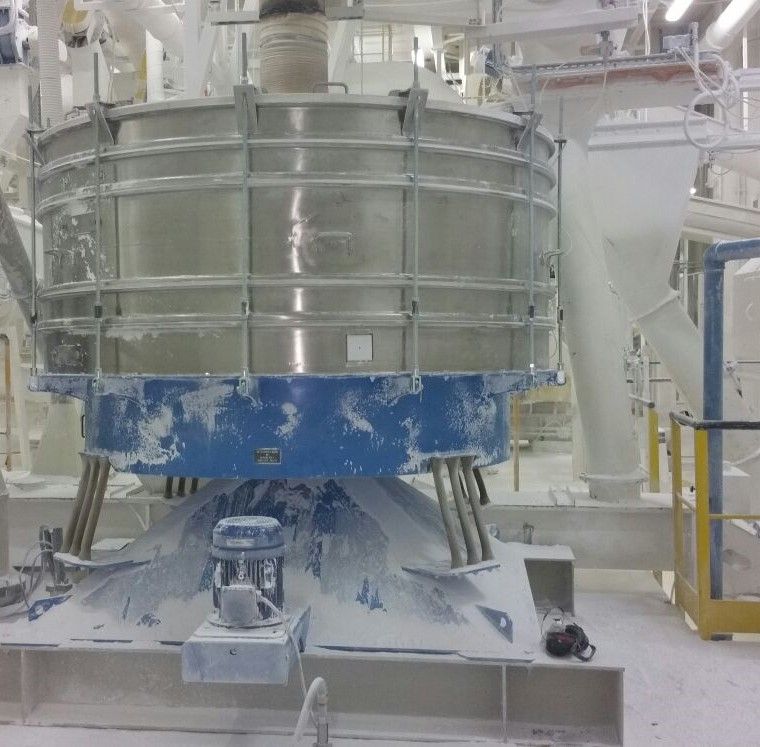
VAN Tumbler Screener
The VAN tumbler screener provides high-efficiency classification for dry and wet products through a three-dimensional tumbling motion.
Technical Advantages:
• Three-Dimensional Motion: The combination of radial and tangential components keeps the material on the mesh surface longer, increasing separation accuracy.
• High Efficiency: Ensures high throughput even for fine powders through extended surface contact.
• Models: Available in multiple sizes such as 48", 60", 72", 90", and 102", enabling high-capacity processing.
• Materials and Cleaning: 304, 316L, or 316Ti stainless steel construction; easy maintenance thanks to quick-disassembly components.
• Performance: Operates with high separation precision and low noise levels.
This system is particularly preferred for the separation of very fine powders and granules and operates with minimal risk of contamination.
VRU Hybrid Rectangular Screener
The VRU hybrid rectangular screener is suitable for very high-volume classification applications thanks to its wide process surface and horizontal vibration components.
Technical Features:
• Screen Structure: The rectangular design provides a larger process area and high efficiency for large feed volumes.
• Vibration Mechanics: Internal eccentric masses generate a combination of horizontal and vertical vibrations, ensuring uniform material movement across the mesh.
• Mesh Replacement: Quick-change mesh system reduces machine downtime.
• Manufacturing Options: Stainless steel body with mesh configurations tailored to specific process conditions.
This model is ideal for production lines requiring high capacity and continuous operation.
Operating Principle and Performance Advantages
Vibrowest classification screens use controlled vibration energy generated by a motor to keep the product in continuous motion across the mesh surface. The combination of horizontal and vertical vibration components enables particle separation according to mesh openings. The system design allows both coarse and fine fractions to be separated within the same unit.
Operational Advantages:
• High-precision classification
• Low energy consumption
• Dust and noise control
• Easy maintenance and cleaning
• Modular structure suitable for process integration
• Compatibility with various mesh types and mesh-cleaning accessories
Fields of Application
Vibrowest classification screens are widely used in the following sectors:
• Food production and process control
• Pharmaceutical and fine powder separation
• Metallic powders and granules
• Fine product classification in the chemical industry
• Recycling material separation
• Agricultural product processing
• Mining and mineral classification
• Plastic granule and polymer powder applications
• Additive manufacturing / 3D powder processes
• Powder coating production
Vibrowest Vibrating Screens for Classification provide high-performance, modular, and customizable classification solutions to enhance process continuity, product quality, and production efficiency. They can be fully designed to match production line requirements in terms of mesh size, body material, vibration characteristics, and additional accessories.